- Home
- About Us
- Products
- News
- Download
- Send Inquiry
- Contact Us
Products
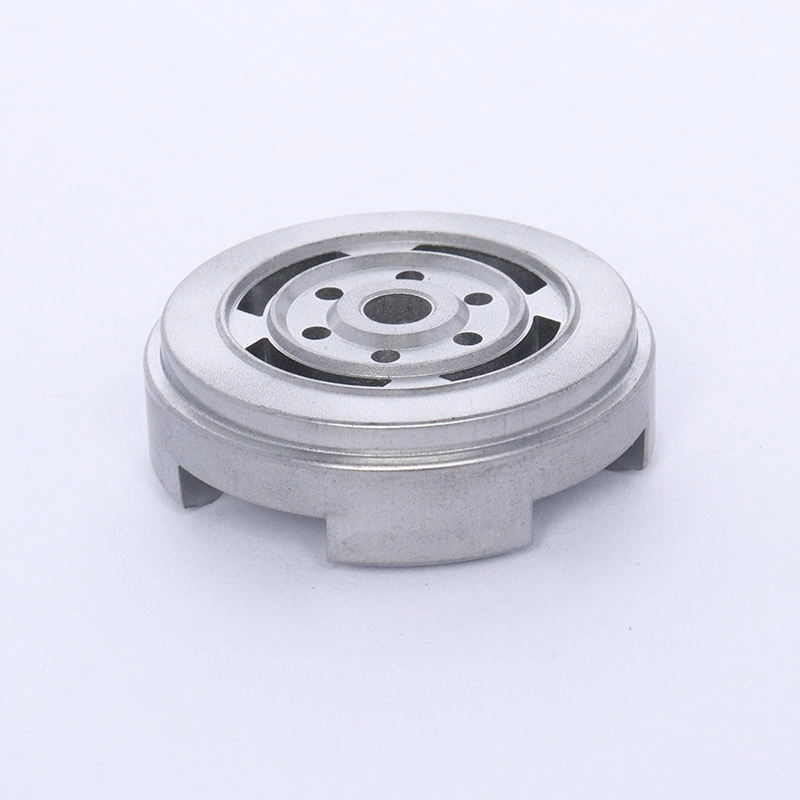
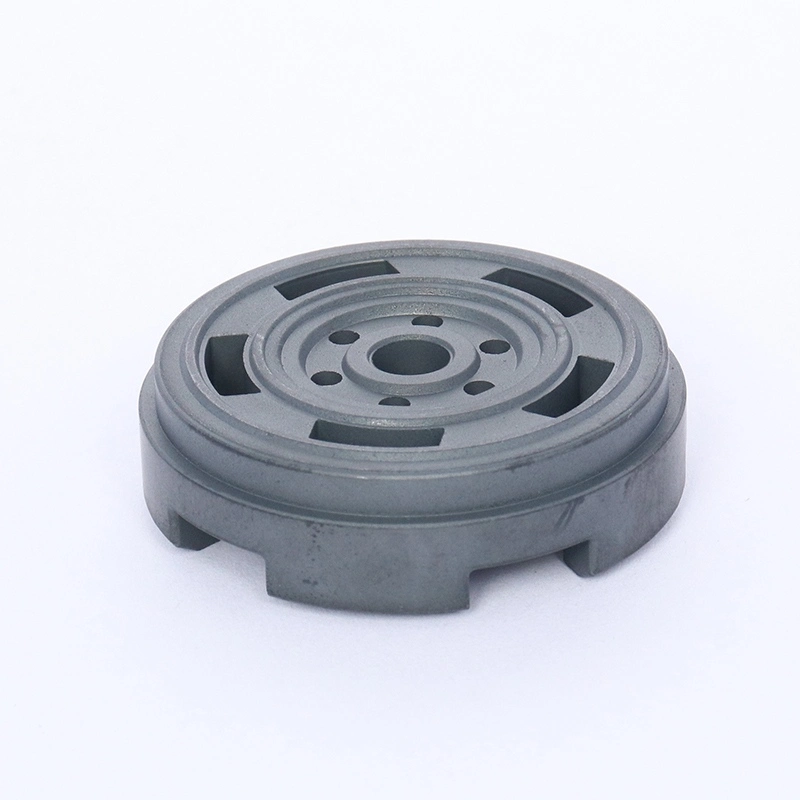
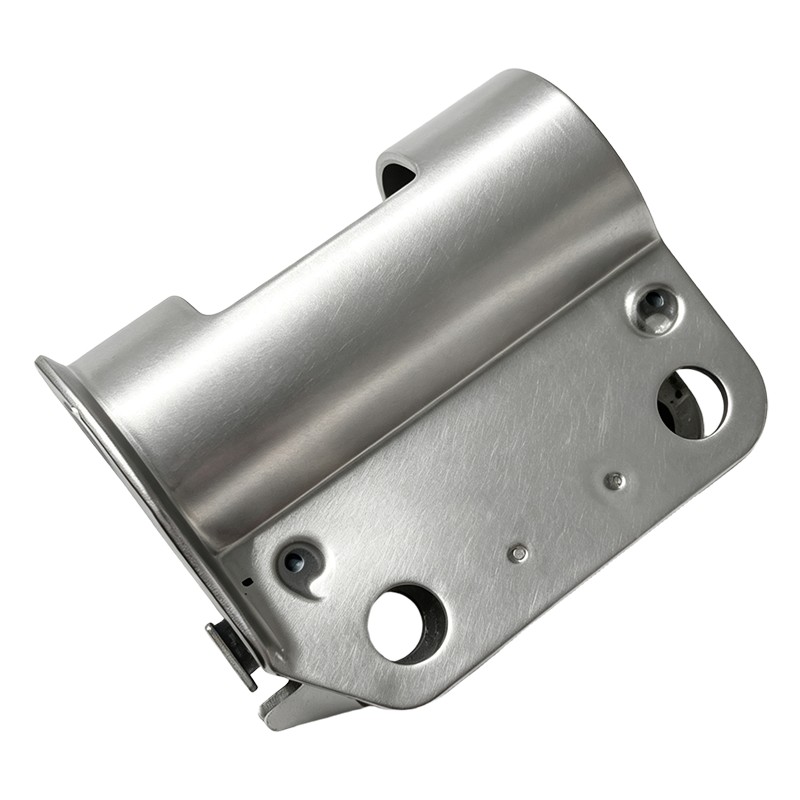
We supply full-category shock absorber components, including pistons, stampings, rubber seals, piston rods, springs, and self-developed banding/grooving machines.
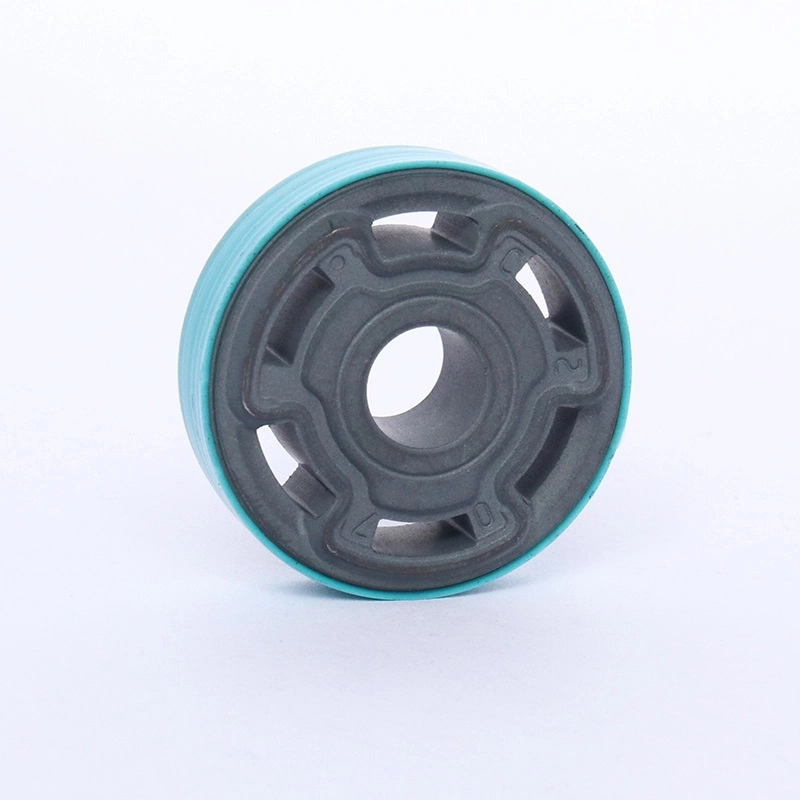
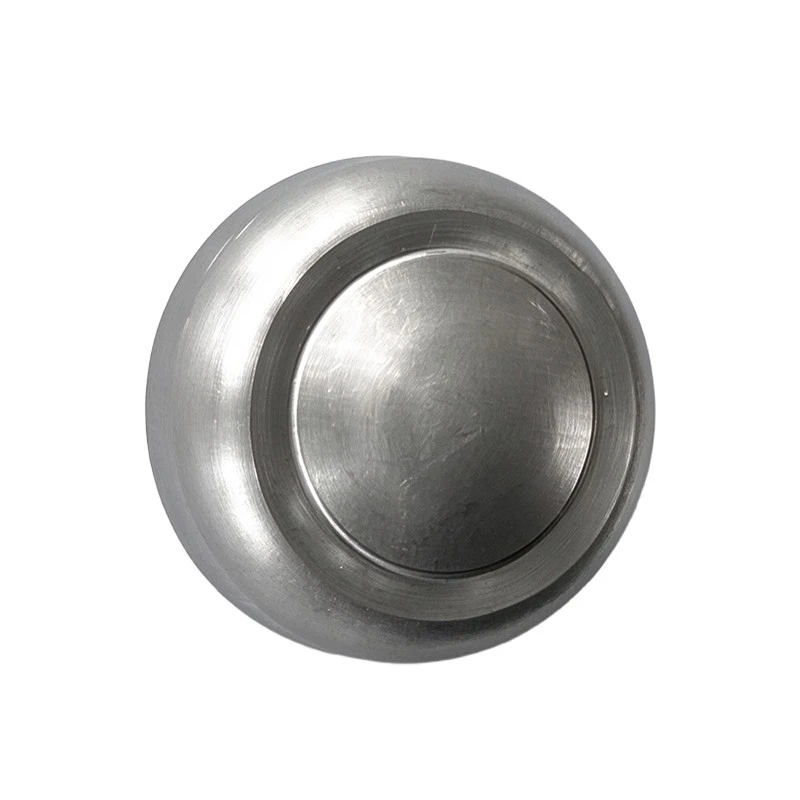
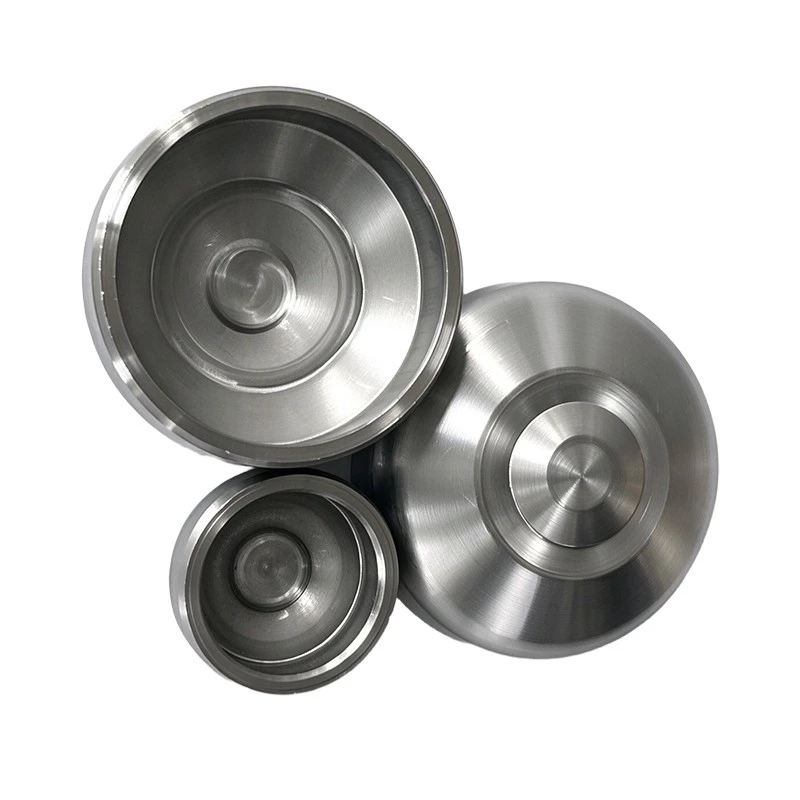
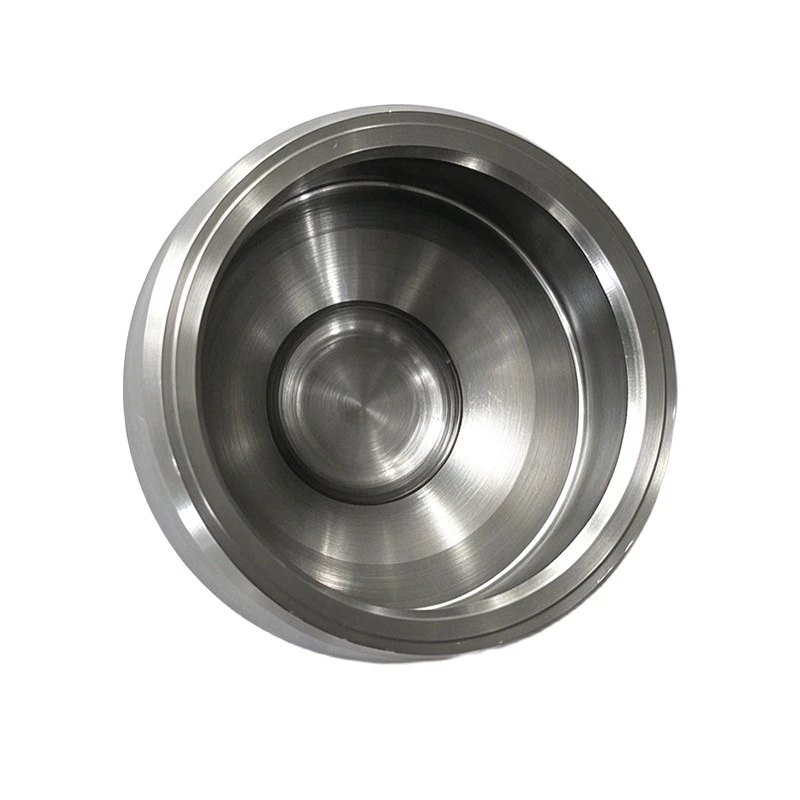
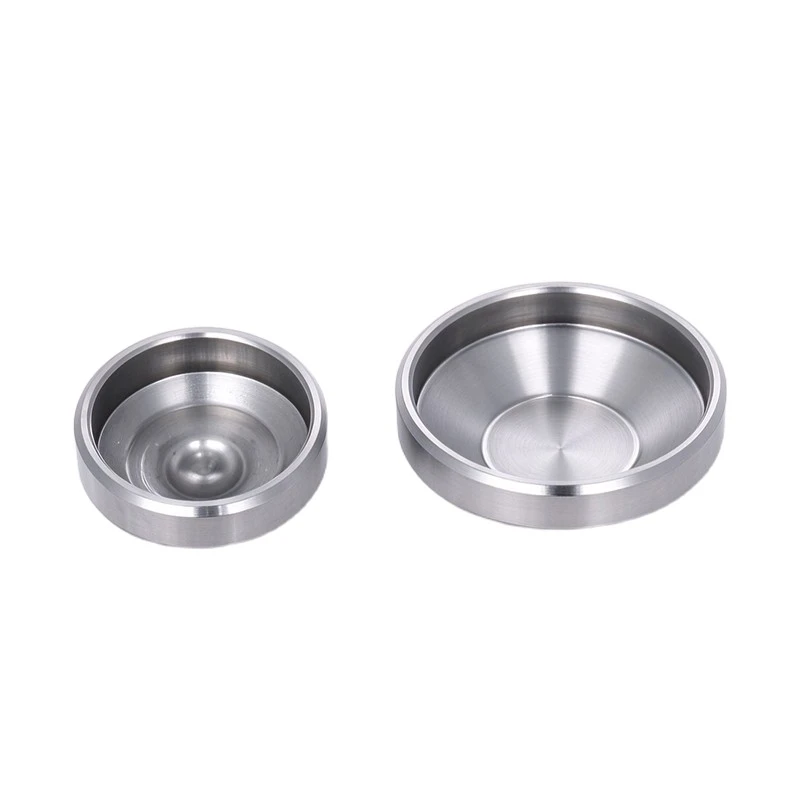
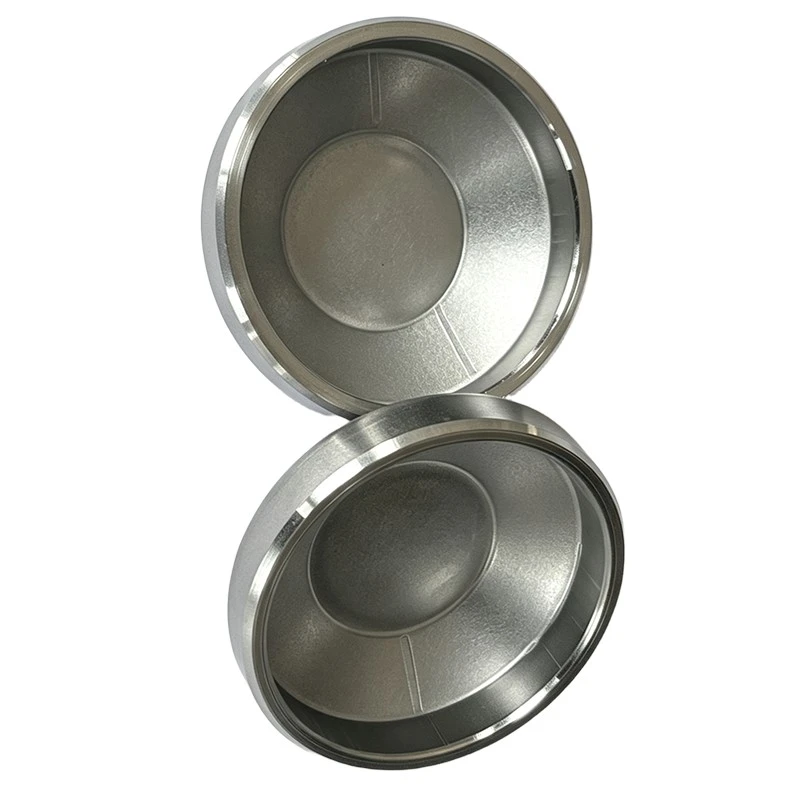
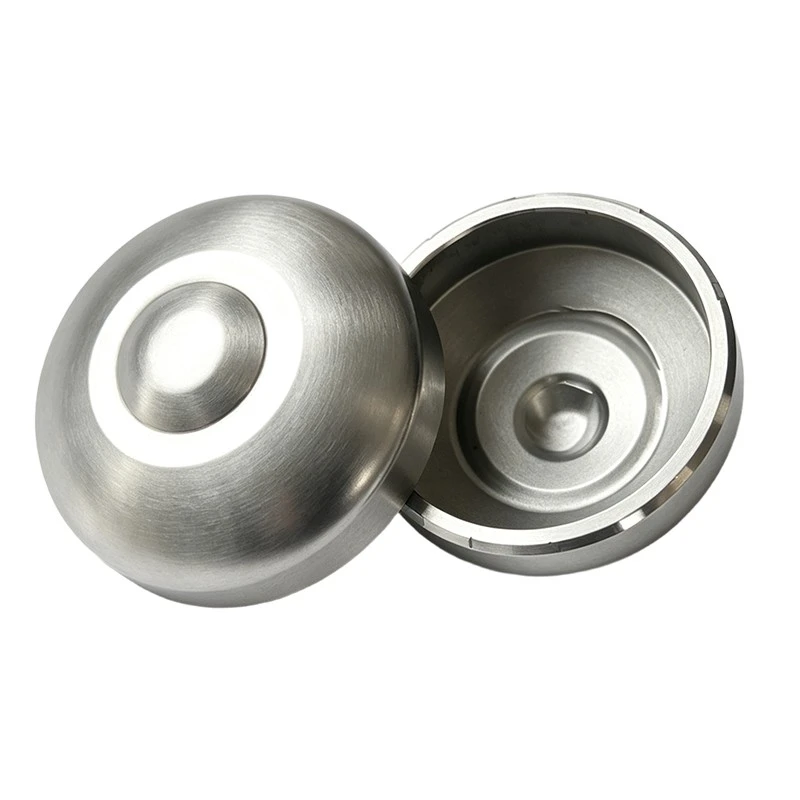
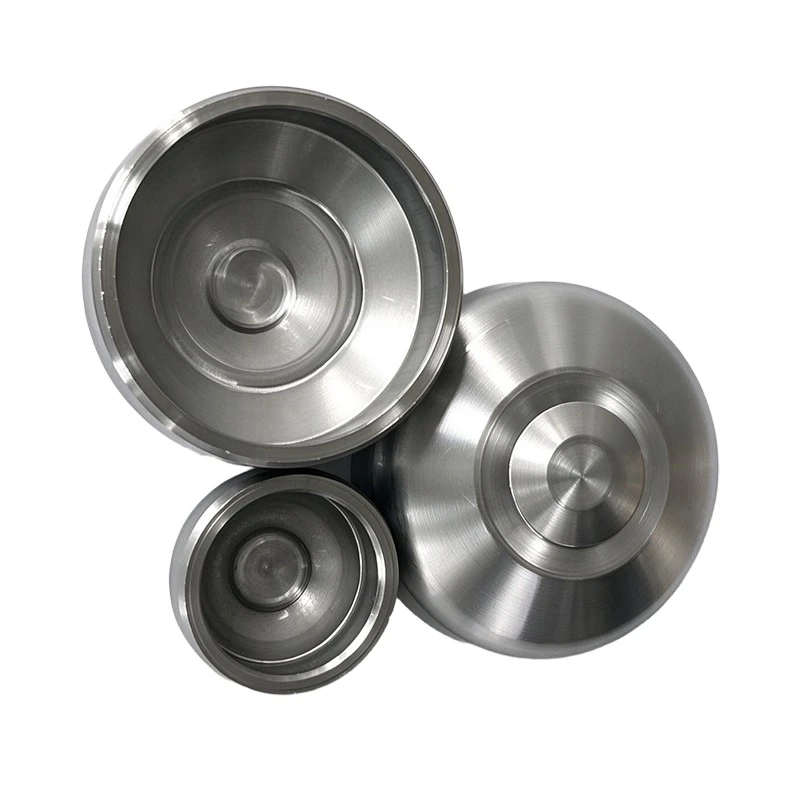
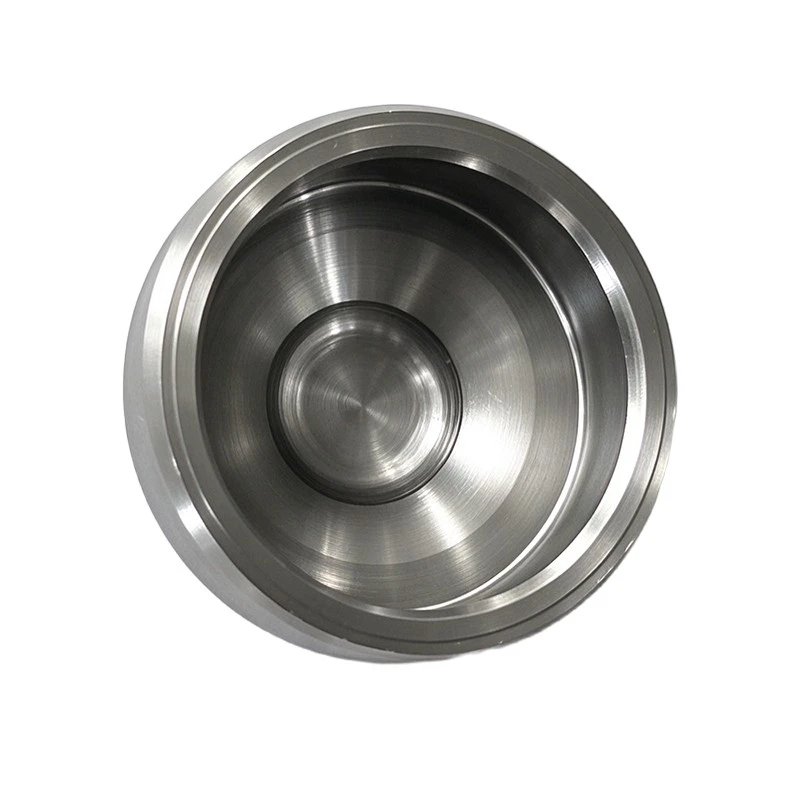
Leak Proof Welded End Cap
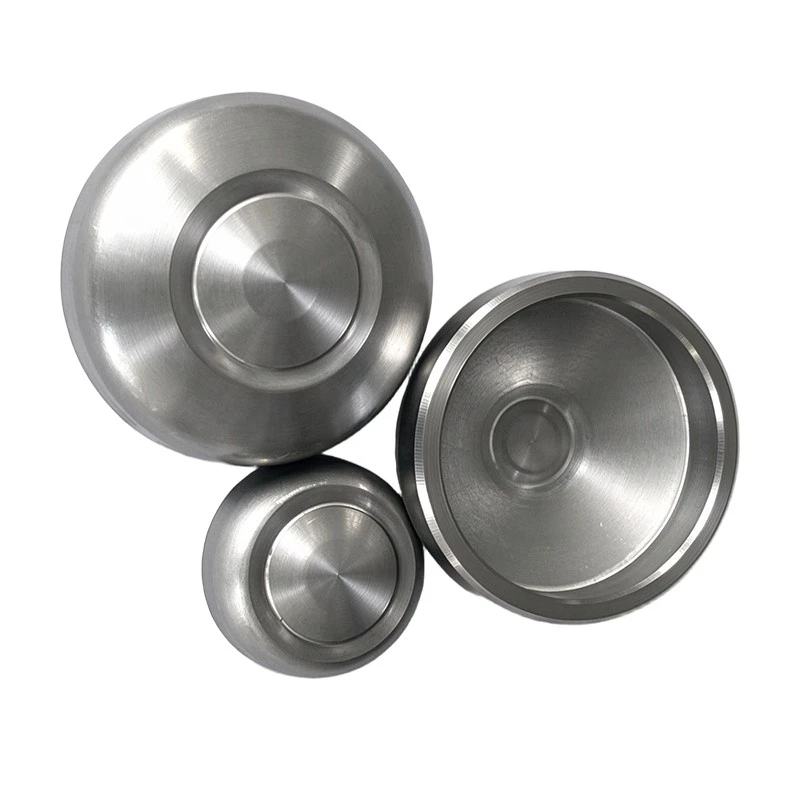
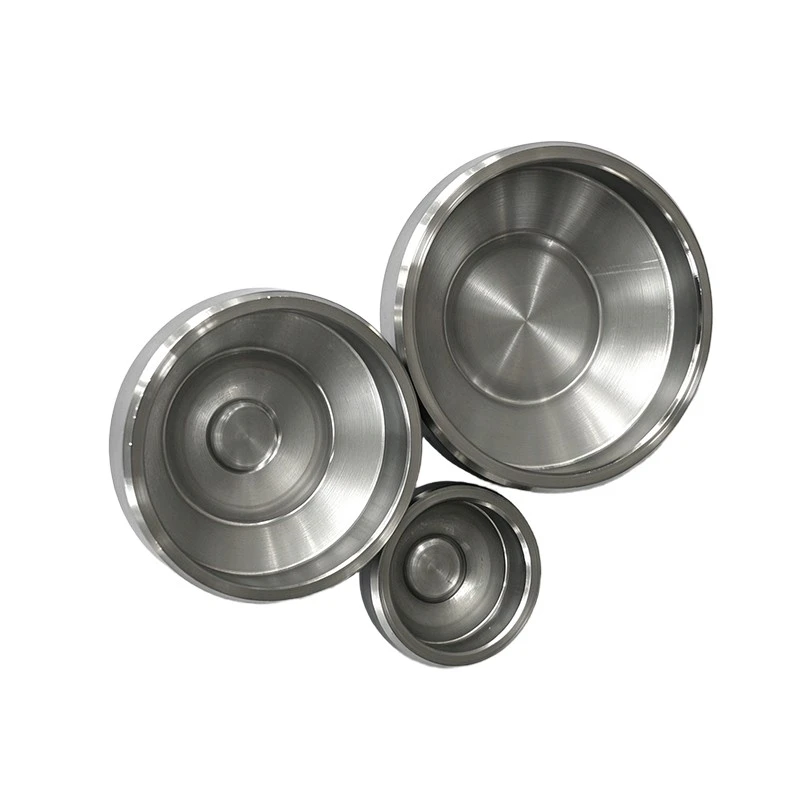
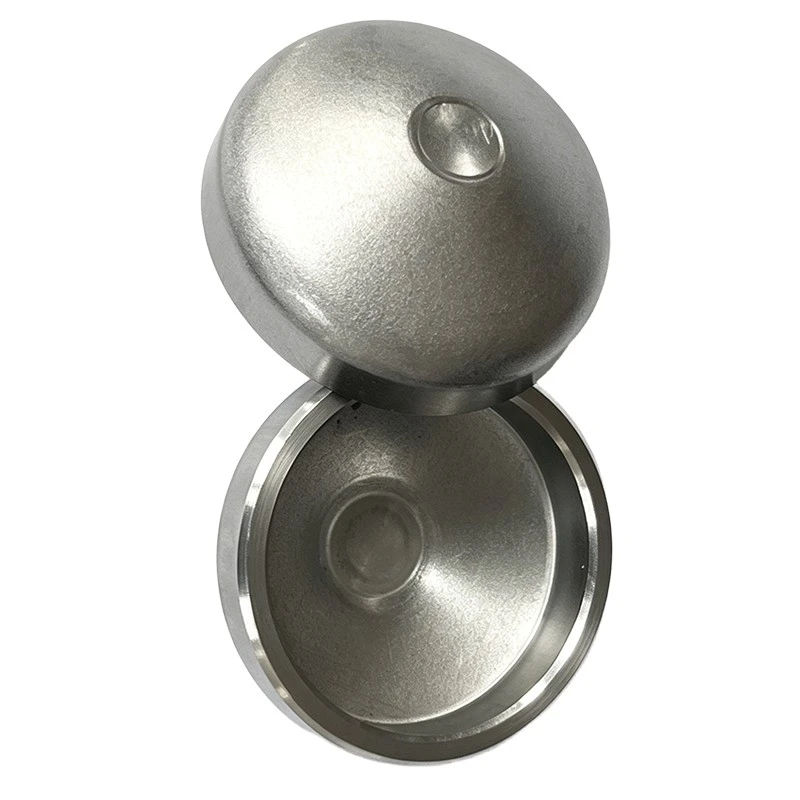
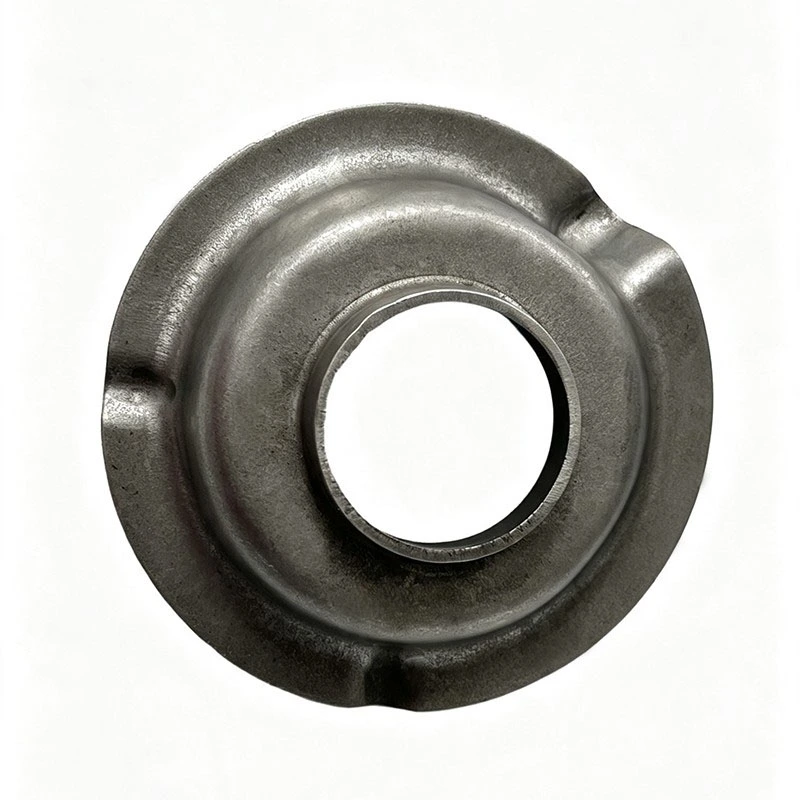
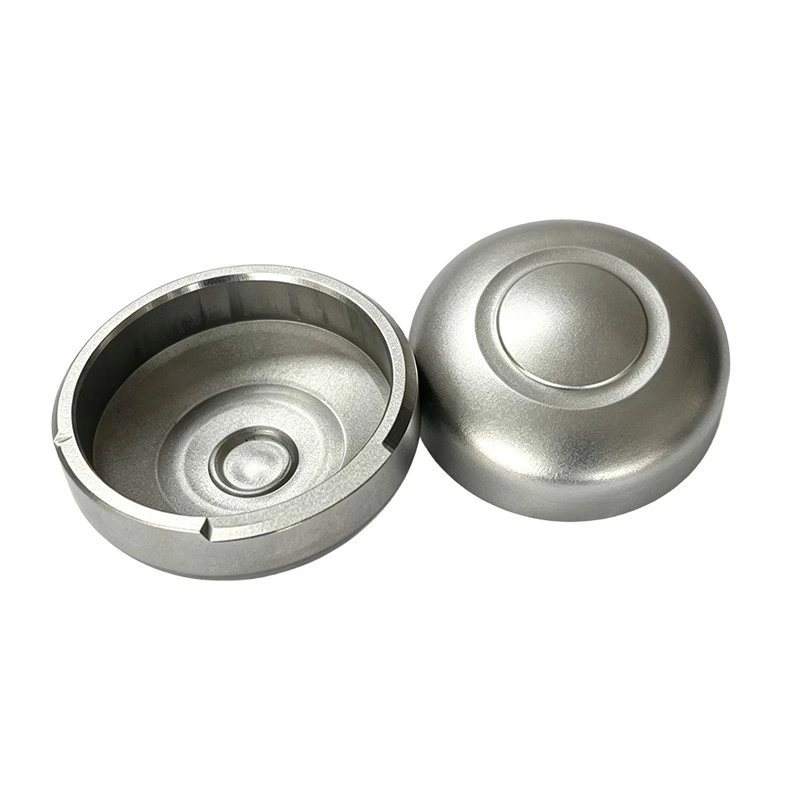
Leak Proof Welded End Cap from XIAYI holds a mirror-polished weld face down to Ra 0.6 μm, and every unit leaves our factory only after passing a 10 bar, 30-second air-tightness test — 100% tested, no sample luck. Fit it once and the cylinder stays dry for the shock's full service life.
Oil leakage is the most expensive failure a shock absorber end cap can produce — it starts with a weld seam that looked fine on the outside. Our Leak Proof Welded End Cap is engineered around one goal: zero hidden leakage channels. The weld end face is CNC machined and mirror polished to Ra ≤ 0.6 μm with end-face flatness held to ≤ 0.03 mm, so the cap and cylinder fuse into a continuous, pore-free seam instead of a patchy weld with micro-gaps.
Every single unit — not a sample, not a batch — passes a 10 bar / 30 s automated air-tightness test with zero pressure drop, followed by batch-sampled hydraulic burst verification at ≥ 50 bar. If a cap cannot hold air, it never reaches your assembly line.
100%
Air-tightness tested, 10 bar / 30 s
≥ 50 bar
Burst pressure, batch verified
Ra ≤ 0.6 μm
Polished weld end face
Where Leaks Actually Come From — And How We Close Each Path
| Leakage Path | Mechanical Root Cause | XIAYI Countermeasure |
|---|---|---|
| Virtual weld / weld seepage | Uneven or rough end face breaks weld fusion | Integrated CNC facing + mirror polishing, verticality controlled |
| Hidden slow leakage | Porosity invisible to visual inspection | 100% automated air leak test on every unit |
| Warp-induced gap after welding | Residual stress releases during cylinder welding heat | Flatness ≤ 0.03 mm verified on laser flatness tester |
| Seepage at flange edge | Eccentric flange, uneven welding gap | Coaxiality ≤ 0.02 mm, 100% laser checked |
Eight-Step Closed-Loop Control, Built Around the Seal
| Step | Control Target |
|---|---|
| 1. Raw material inspection | Special deep-drawing steel, thickness tolerance ±0.05 mm, no oil / rust / warp |
| 2. Leveling & slitting | Burr-free, chip-free edges — no tool scratch carried into forming |
| 3. Multi-stage deep drawing | Wall thickness difference ≤ 0.08 mm, no wrinkle or necking |
| 4. Flanging & trimming | R1.8–R2.5 flange, coaxiality ≤ 0.025 mm, no stress concentration |
| 5. End facing & polishing | Flatness ≤ 0.03 mm, weld surface Ra ≤ 0.6 μm, vertical end face |
| 6. Pre-treatment & coating | Composite coating 40–65 μm, adhesion grade 0 |
| 7. Full performance inspection | Dimensions + air tightness + pressure resistance, 100% coverage |
| 8. Dust-proof packaging & coding | Laser traceability code per unit, moisture-proof individual packing |
Seal-Related Testing Equipment
| Test | Equipment | Acceptance Standard | Frequency |
|---|---|---|---|
| Air tightness | Auto Air Leak Tester | 10 bar / 30 s, zero pressure drop | 100% |
| Pressure resistance | Hydraulic Burst Tester | Burst ≥ 50 bar | Batch sampling |
| Flatness & coaxiality | Laser Flatness & Coaxiality Tester | ≤ 0.02 mm | 100% |
| Weld surface finish | CNC Lathe & Polisher line | Ra ≤ 0.6 μm | Per shift |
Why B Buyers Choose a Tested Cap
For shock absorber assemblers, a field leakage claim costs far more than the cap itself: cylinder returns, warranty handling, and lost line confidence. A cap that has passed 100% air tightness and pressure verification removes the single most common early-failure mode from your risk list — before it ever reaches the welding robot.
FAQ
Q: Can you match our cylinder inner diameter and welding parameters?
A: Yes. Send us your cylinder drawing or a sample cap; we match fitting outer diameter, flange profile and end-face finish, then confirm weldability with trial welding before mass production.
Q: Is the 10 bar / 30 s test really applied to every piece?
A: Yes — the automated air leak tester runs inline at 100% frequency, and any pressure drop automatically diverts the unit off the line. Batch data is retained for traceability.
Q: What coating do you recommend for leak-critical applications?
A: For weld-critical parts we recommend cathodic e-coat, whose film builds evenly (20–30 μm) without interfering with welding; heavier powder systems are available for corrosion-first environments.
Request leak-test reports and samples for your cylinder program
Ningbo XiaYi Electromechanical Tech Co., Ltd. — IATF 16949:2016 certified shock absorber stamping parts manufacturer in Ningbo, Zhejiang. Share your drawings for a fast quotation and trial-welding validation.
About XIAYI seal reliability: XIAYI runs an in-house seal verification station where automated air-tightness testing, hydraulic burst verification and laser geometry checking operate on the same line as production — inspection data feeds directly back into process parameters, so a drifting dimension is corrected the same shift it appears, not after a customer complaint.
Hot Tags: Leak Proof Welded End Cap, China, Manufacturer, Supplier, Factory
Send Inquiry
Contact Info
-
Address
No.209 Lane 520 Tongning Rd,Qianjiang Street,Jiangbei District, Ningbo City, Zhejiang Province, China
-
Tel
-
Email
Get a Tailored Quote for Your Shock Absorber Parts
Why Global Buyers Choose Ningbo Xiayi:
✓ IATF 16949 Certified — Defect rate strictly controlled below 0.1%.
✓ Full-Category Supply — Pistons, rods, springs, stampings & rubber parts.
✓ R&D Support — Custom powder metallurgy formulas & 7-10 day rapid prototyping.
✓ Proven Capacity — 50 million core pistons produced annually for global OEMs.
Ready to start? Complete the form below and our engineering team will respond within 24 hours with a custom recommendation.