- Home
- About Us
- Products
- News
- Download
- Send Inquiry
- Contact Us
Products
We supply full-category shock absorber components, including pistons, stampings, rubber seals, piston rods, springs, and self-developed banding/grooving machines.
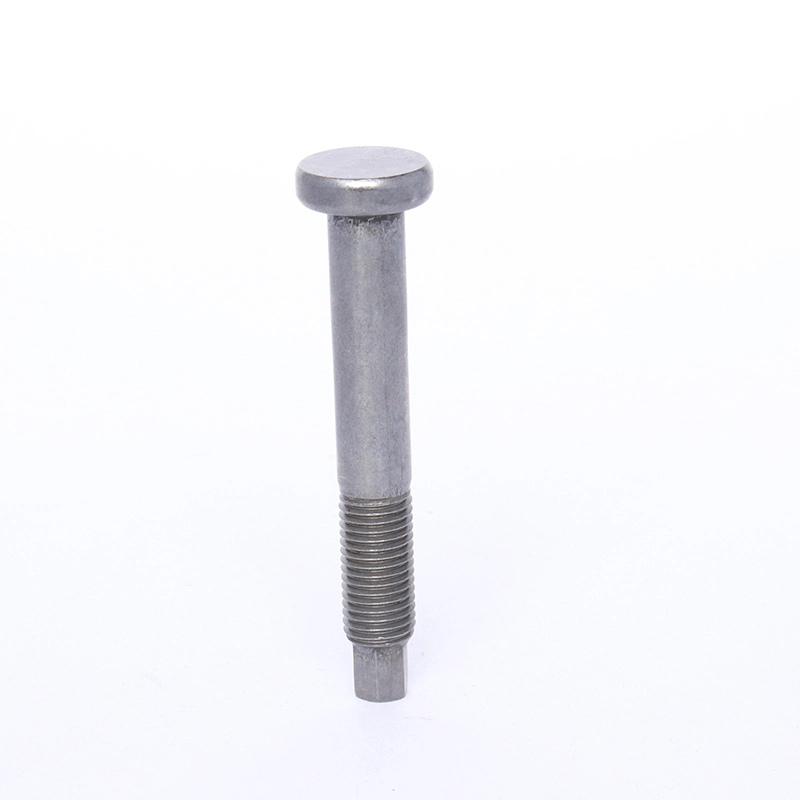
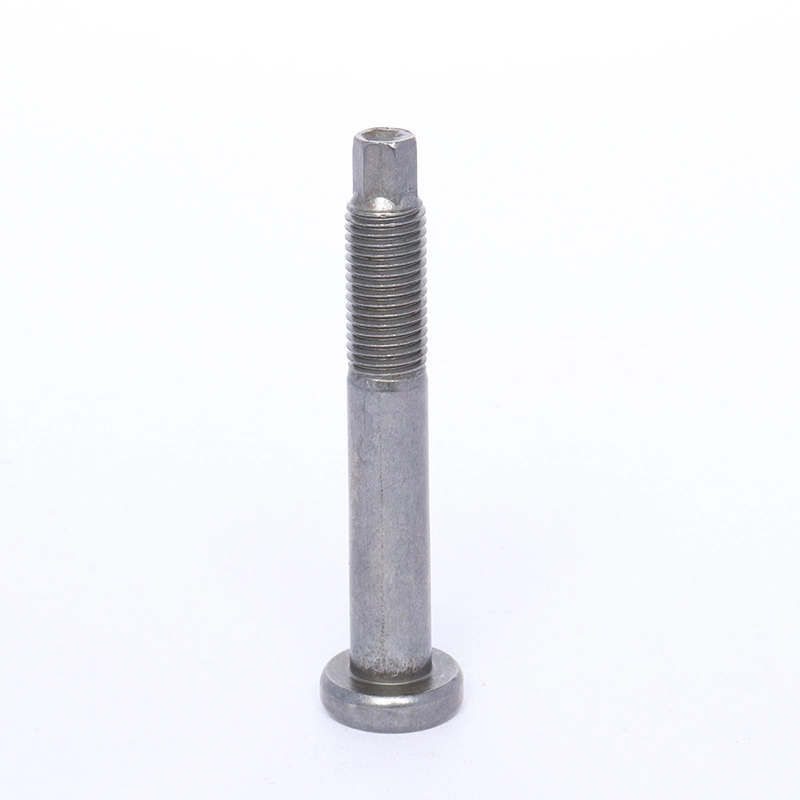
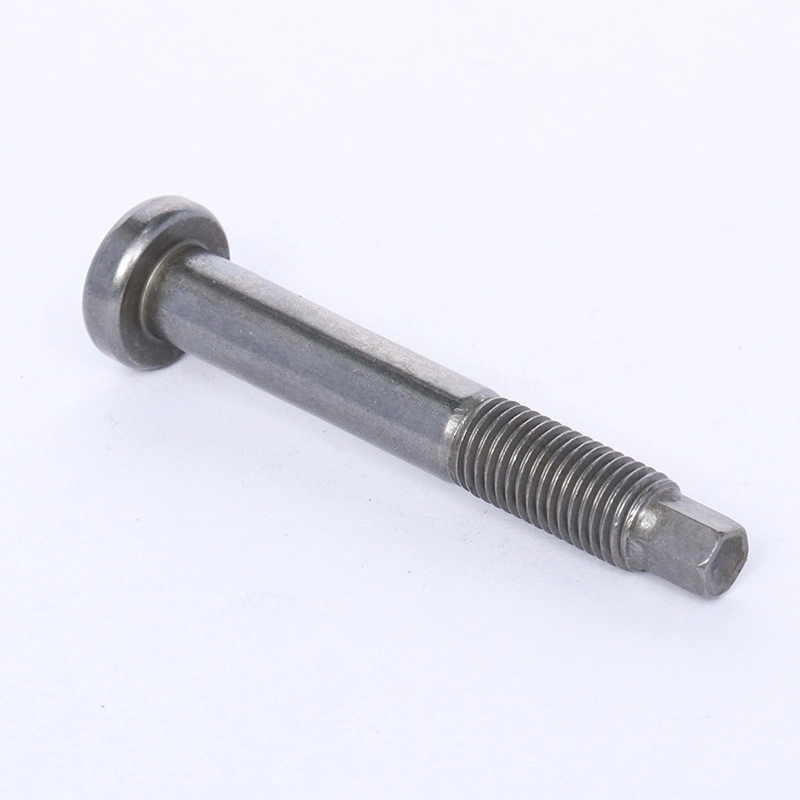
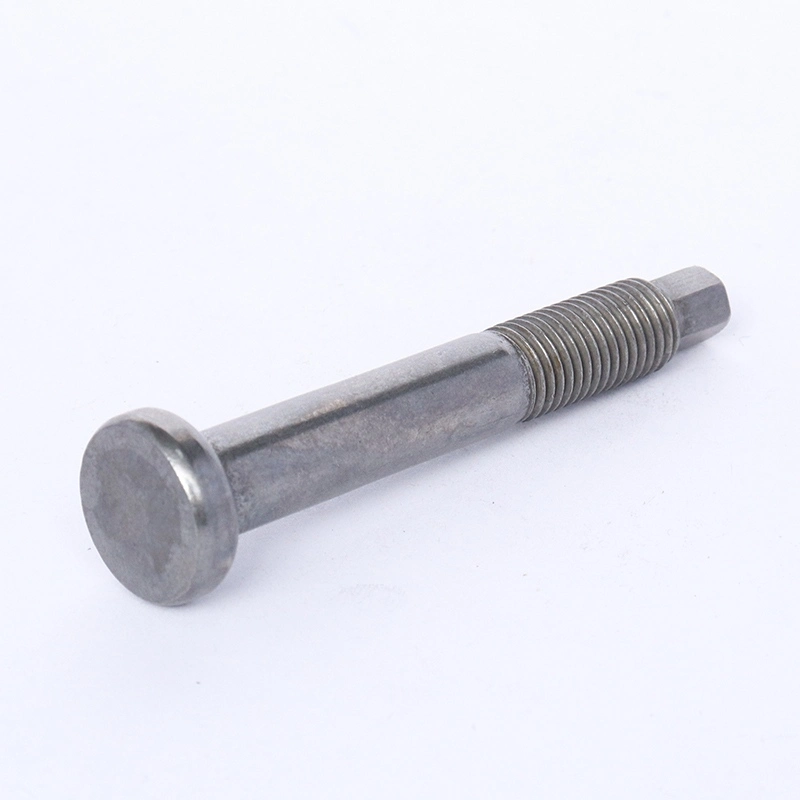
Heat-Treated Shock Absorber Bolt
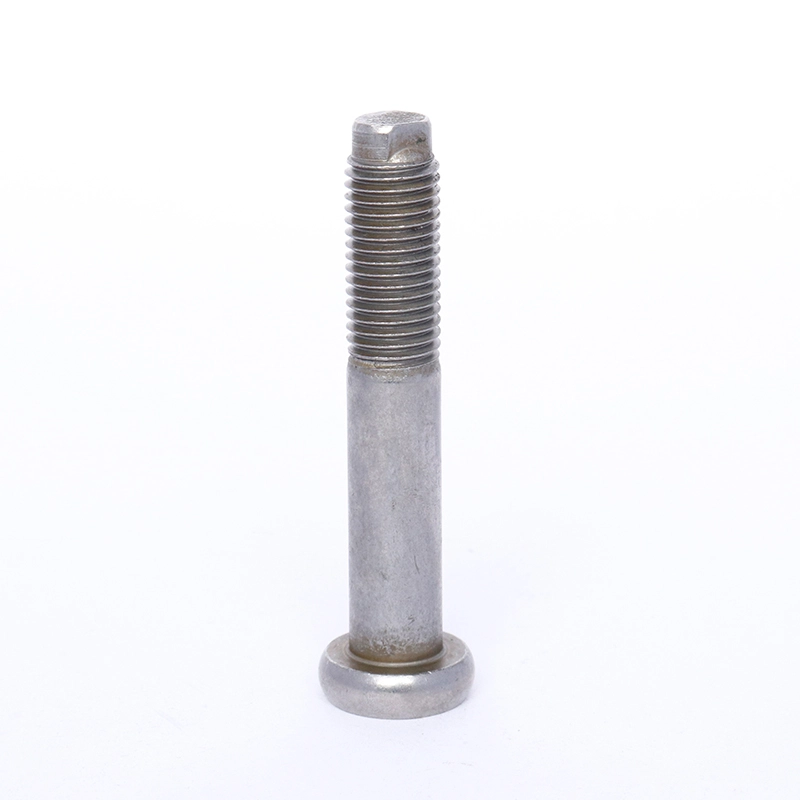
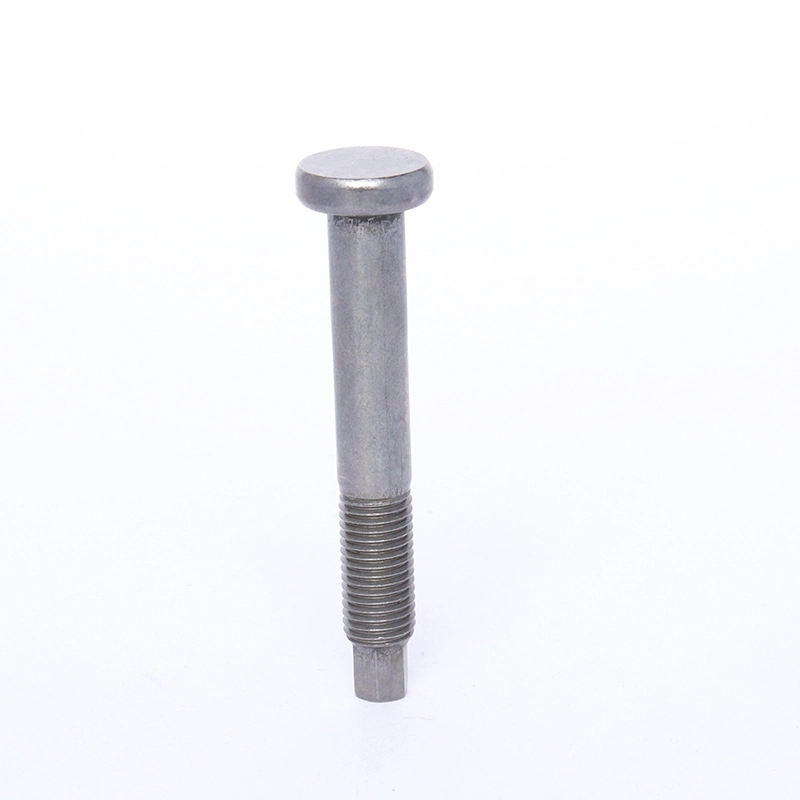
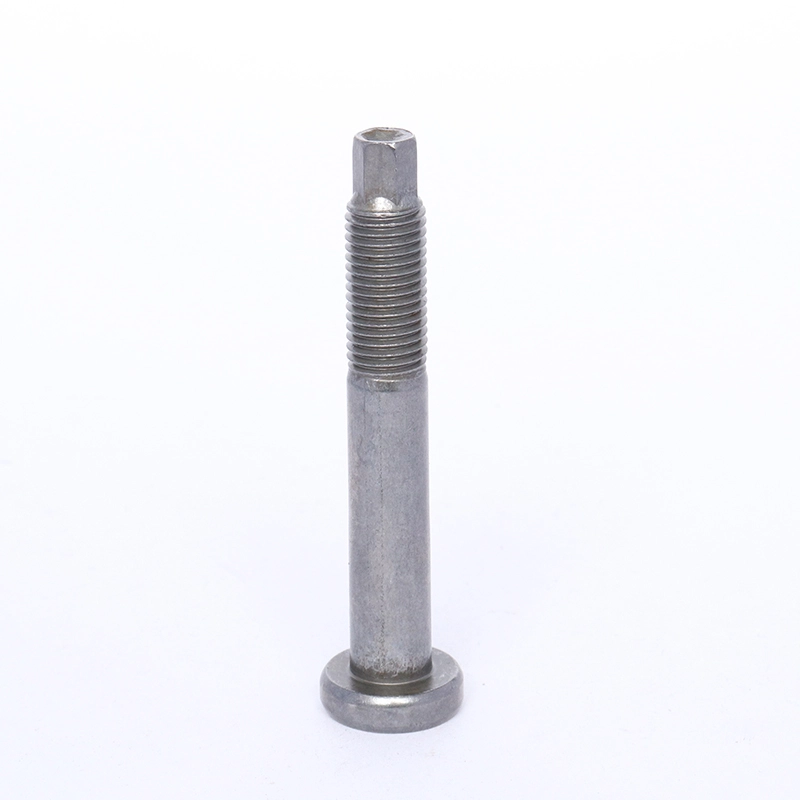
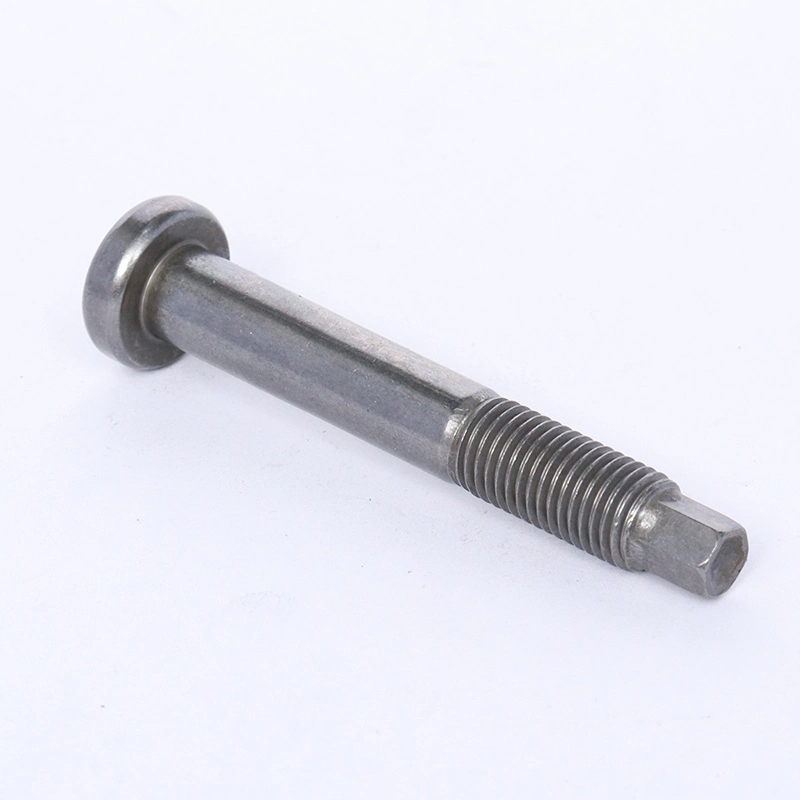
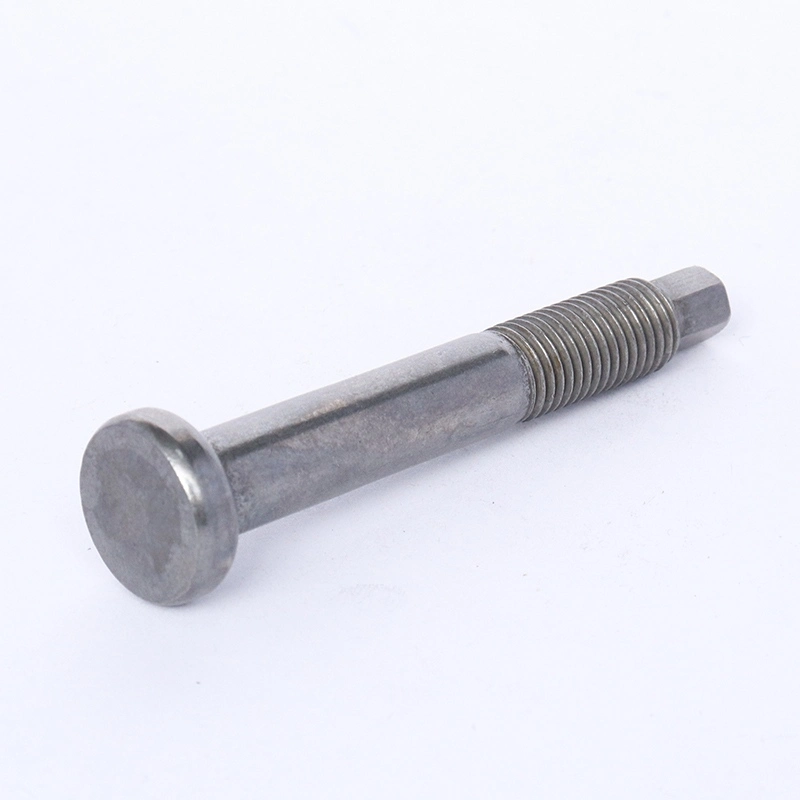
XIAYI Heat-Treated Shock Absorber Bolt is a precision limit fastener developed for shock absorber piston rod reciprocating movement, damping valve positioning, and hydraulic stroke limitation. It is manufactured from 40Cr alloy steel and processed through four-section integrated cold forging, vacuum quenching and tempering, precision turning, thread rolling, and multi-layer anti-corrosion passivation.
XIAYI has established a quality management system compliant with IATF 16949:2016, supporting controlled production, batch inspection, and traceability for automotive fasteners. The Heat-Treated Shock Absorber Bolt is suitable for OEM shock absorber production, aftermarket replacement, modified suspension systems, passenger cars, SUVs, light trucks, and selected engineering equipment.
Selection Based on Working Conditions
Reciprocating Movement
The smooth middle shank is precision turned to a surface roughness of Ra≤0.2μm. By separating the moving surface from the threaded section, the design minimizes repeated contact between thread crests and the shock absorber oil seal. This structure is suitable for applications where the piston rod repeatedly extends and retracts over long operating periods, helping reduce unnecessary friction between the fastener and sealing components.
Dynamic Loading
The 40Cr alloy steel body undergoes vacuum quenching at approximately 880°C followed by tempering at approximately 520°C. The controlled process reduces surface decarburization and provides a target hardness range of 32--38 HRC. The resulting combination of strength and toughness is designed to resist shaft bending, thread deformation, and fatigue damage under alternating vibration loads.
Automatic Assembly
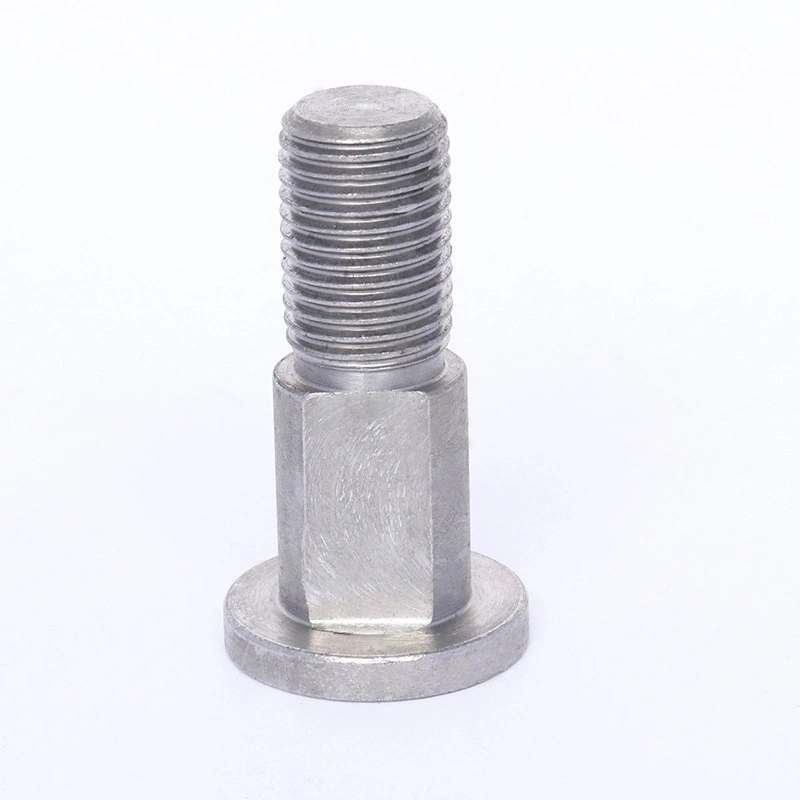
The integrated square lug at the bottom of the bolt engages with the corresponding limit structure of the shock absorber valve body. It provides anti-rotation during tightening without requiring separate holding tools. For high-volume production, this structure can reduce manual intervention and improve compatibility with automated tightening equipment.
Structural Configuration
The Heat-Treated Shock Absorber Bolt uses different functional sections rather than relying on a conventional full-thread shaft.
| Section | Design | Purpose |
|---|---|---|
| Round head | 0.8 mm R arc transition | Reduces sharp edges and assembly damage |
| Smooth shank | Ra≤0.2μm mirror-finished surface | Limits friction against sealing components |
| Threaded section | Bottom segmented metric thread | Keeps threads away from reciprocating seal contact |
| Anti-rotation lug | Integrated square lug, tolerance ±0.02 mm | Prevents bolt rotation during tightening |
| Main body | 40Cr alloy steel | Provides strength and fatigue resistance |
This configuration allows the fastener to perform both as a mechanical limit component and as a precision interface component inside the shock absorber assembly.
Manufacturing and Quality Verification
Forming Accuracy
The round head is produced through progressive cold forging with a controlled arc transition. The smooth shank is subsequently precision turned to remove tool marks and surface irregularities. Dimensional targets include a round head diameter tolerance of ±0.03 mm, smooth shank diameter tolerance of ±0.01 mm, square lug tolerance of ±0.02 mm, overall length tolerance of ±0.2 mm, and overall coaxiality of ≤0.03 mm. These controls help maintain consistent positioning during shock absorber assembly.
Heat Treatment Control
Vacuum quenching and tempering are used to obtain consistent mechanical properties throughout the fastener body. The standard acceptance requirements include 40Cr alloy steel material, hardness of 32--38 HRC, tensile strength of at least 1040 MPa, yield strength of at least 940 MPa, and salt spray resistance of at least 500 hours. The integral forged construction also eliminates welding seams that could otherwise become potential structural weak points.
Surface and Corrosion Protection
The fastener uses multi-layer galvanizing and sealing passivation to improve resistance to moisture, road salt, mud, and other underbody contaminants. A 500-hour neutral salt spray test is used to verify corrosion resistance. This is particularly relevant for vehicles operated in coastal areas, snowy regions, or environments where road de-icing salt is frequently used.
Inspection Equipment
Quality verification is performed using dedicated inspection equipment rather than relying only on final visual inspection.
| Equipment | Inspection Scope | Quality Purpose |
|---|---|---|
| Optical inspection machine | Burrs, head radius, lug | Detects forming defects |
| 3D coordinate measuring machine | Overall dimensions and geometry | Verifies dimensional consistency |
| Thread Go/No-Go tester | Thread tolerance and engagement | Prevents assembly interference |
| Heat treatment tester | Hardness and mechanical properties | Confirms treatment consistency |
| Salt spray chamber | Corrosion resistance | Verifies surface protection |
| Reciprocating wear tester | Simulated friction cycles | Evaluates shank surface performance |
The inspection process is designed to identify dimensional, structural, surface, and mechanical defects before products enter customer assembly lines.
Application Matching
The Heat-Treated Shock Absorber Bolt can be selected according to shock absorber structure and operating conditions.
| Application | Typical Working Condition | Recommended Configuration |
|---|---|---|
| Passenger car shock absorbers | Daily road driving and highway operation | Half-thread structure with smooth shank |
| SUV suspension | Higher suspension travel and vehicle load | Heat-treated body with reinforced limit section |
| Modified adjustable shocks | Repeated adjustment and dynamic loading | Precision shank and anti-rotation lug |
| Light trucks | Higher vibration and payload | 40Cr vacuum-treated structure |
| Hydraulic stroke limitation | Repeated reciprocating movement | Smooth shank with segmented thread |
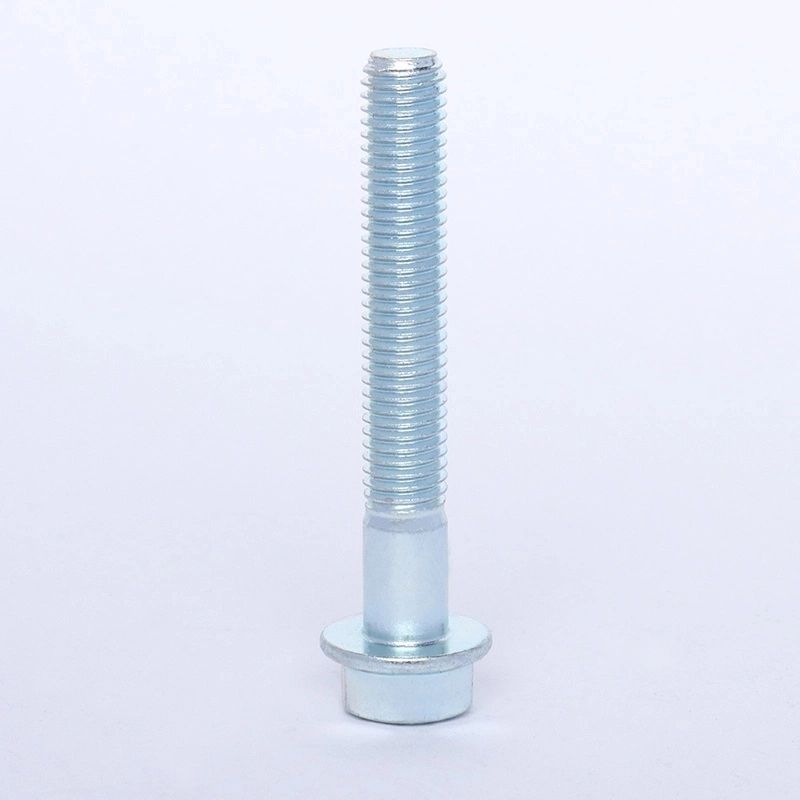
The full-thread structure is more appropriate for static fastening applications where there is no continuous reciprocating contact with an oil seal. For dynamic shock absorber applications, the smooth-shank configuration provides a more suitable interface.
Real Application Engineering Case
In early 2025, a domestic professional shock absorber OEM manufacturer comprehensively upgraded its piston rod limit fasteners with XIAYI Heat-Treated Shock Absorber Bolts.
The original ordinary non-standard pin bolts used simple air furnace heat treatment and had inconsistent hardness, rough shank surfaces, and no anti-rotation structure. During mass production and vehicle road testing, the customer encountered several problems, including low assembly efficiency requiring manual anti-rotation assistance, oil seal scratching and early leakage after 20,000--30,000 km, and occasional bolt bending after prolonged mountain-road vibration.
After replacing the original fasteners with the XIAYI solution, the customer reported significant improvements. Standard vacuum tempering heat treatment ensured more consistent hardness and toughness, with zero stroke failure reported after a 100,000 km road test. The mirror-finished shank and arc burr-free structure reduced oil seal damage, while the average service life of the shock absorber increased by 55%. The integrated square anti-rotation lug allowed fully automatic assembly, increasing production line efficiency by 38%. Stable batch heat treatment and full inspection also reduced fastener-related defects by 85%.
Assembly Considerations
Correct installation is important because the component works directly with the shock absorber's sealing and valve structures.
Positioning
During installation, align the square anti-rotation lug with the corresponding limit groove in the shock absorber valve body. This allows the fastener to remain stationary during tightening and reduces the need for additional manual holding tools.
Orientation
The arc round head should face the specified oil-seal side according to the shock absorber assembly design. Incorrect orientation can create unwanted contact with surrounding components and may affect sealing performance during operation.
Tightening
Use the torque specified by the shock absorber manufacturer. Progressive tightening is recommended instead of excessive one-step tightening, which can damage threads or deform mating components.
Thread Matching
The mating nut or threaded component should match the specified thread tolerance. Using an incompatible thread can cause poor engagement, thread damage, or automated assembly interference.
Storage
Finished fasteners should be stored in dry, sealed packaging to protect the passivation layer from moisture and oxidation during transportation and long-term storage.
Frequently Asked Questions
What makes this fastener different from a standard shock absorber bolt?
It combines a smooth shank, segmented half-thread, integrated anti-rotation lug, and vacuum heat treatment. The structure is designed for the reciprocating movement and sealing requirements of shock absorbers.
Why is a smooth shank important?
The smooth shank has a surface roughness of Ra≤0.2μm, helping reduce friction and wear against the oil seal during repeated piston movement.
Can XIAYI produce customized dimensions?
Yes. XIAYI supports customization of head diameter, shank length, thread specification, square lug dimensions, hardness, and surface treatment according to customer drawings or application requirements.
Can test reports be supplied for OEM projects?
Yes. XIAYI can provide inspection records for dimensions, hardness, mechanical performance, salt spray resistance, and other agreed quality requirements for OEM projects.
What applications are suitable for this product?
It is mainly used in automotive shock absorbers and suspension systems, as well as selected hydraulic and reciprocating mechanical applications requiring a precision limit fastener.
XIAYI Manufacturing Capability
XIAYI is a China-based manufacturer specializing in customized automotive precision fasteners and heat-treated components. With approximately 12 years of experience, the factory integrates cold forging, vacuum heat treatment, precision machining, surface treatment, and quality inspection. Its quality management system complies with IATF 16949:2016, with a production capacity of approximately 750,000 pieces per day to support OEM, aftermarket, and customized batch orders.
Hot Tags: Heat-Treated Shock Absorber Bolt Manufacturer, Heat-Treated Shock Absorber Bolt Supplier, Heat-Treated Shock Absorber Bolt Wholesale
Related Category
Send Inquiry
Contact Info
-
Address
No.209 Lane 520 Tongning Rd,Qianjiang Street,Jiangbei District, Ningbo City, Zhejiang Province, China
-
Tel
-
Email
Get a Tailored Quote for Your Shock Absorber Parts
Why Global Buyers Choose Ningbo Xiayi:
✓ IATF 16949 Certified — Defect rate strictly controlled below 0.1%.
✓ Full-Category Supply — Pistons, rods, springs, stampings & rubber parts.
✓ R&D Support — Custom powder metallurgy formulas & 7-10 day rapid prototyping.
✓ Proven Capacity — 50 million core pistons produced annually for global OEMs.
Ready to start? Complete the form below and our engineering team will respond within 24 hours with a custom recommendation.